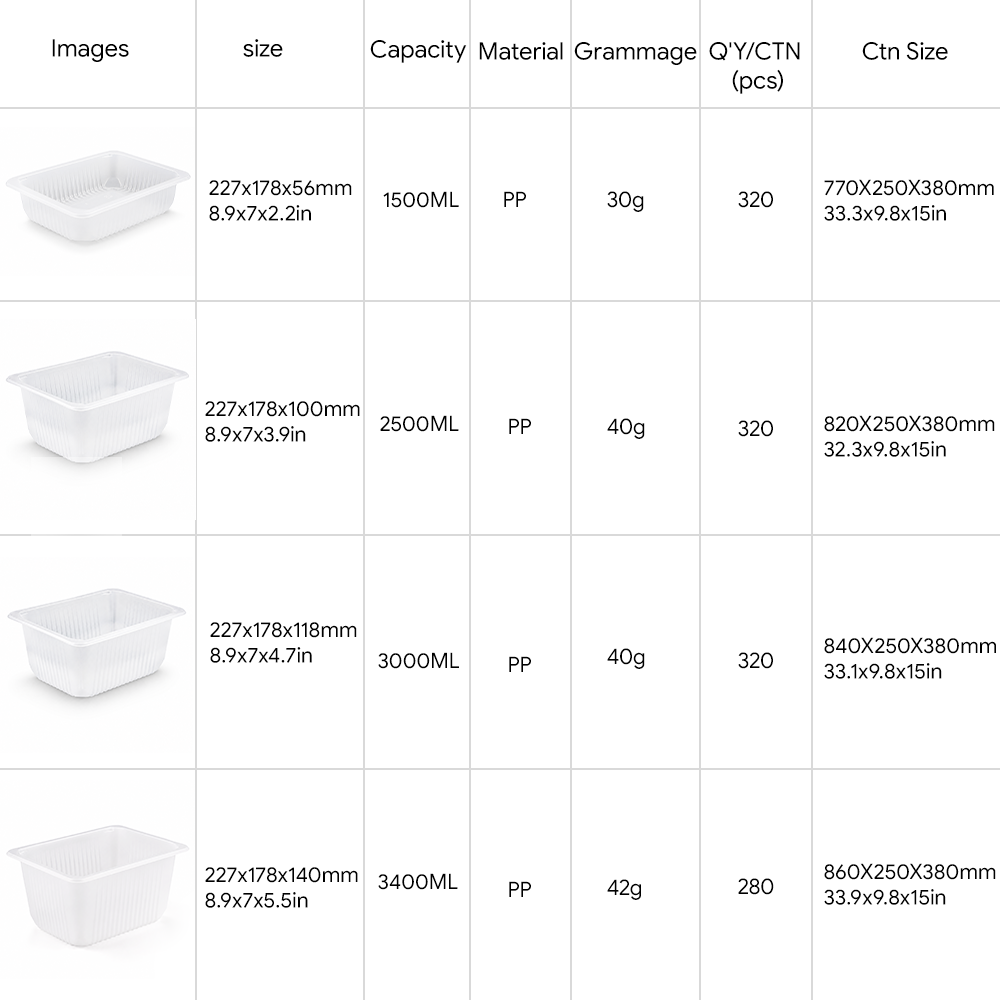
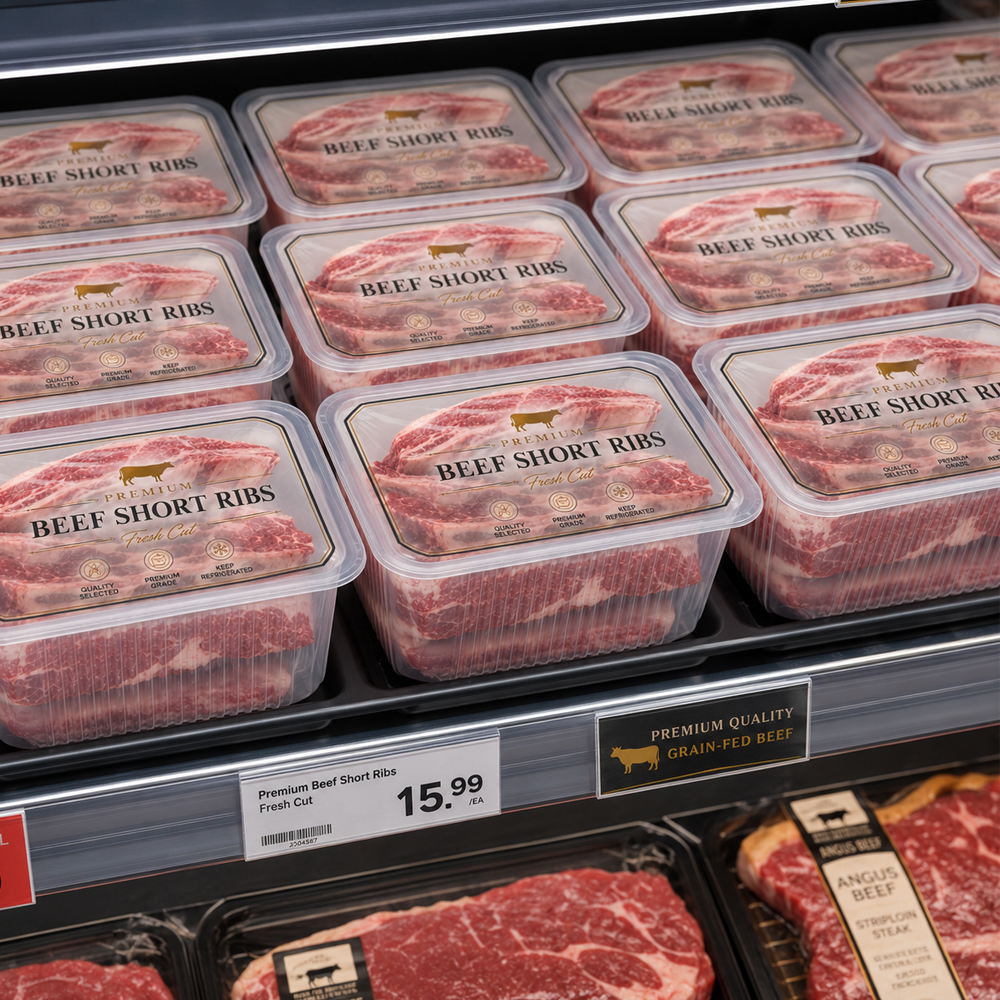
In the realm of food packaging, a vacuum pack sealer is an essential tool for businesses seeking to preserve product freshness, extend shelf life, and enhance presentation. As a purchasing manager or distributor, your primary concerns likely revolve around quality, efficiency, and cost-effectiveness. This article will guide you through the key specifications, evaluation criteria, sourcing options, cost considerations, and diverse applications of vacuum pack sealers, enabling you to make informed purchasing decisions.
How to Evaluate the Quality of Vacuum Pack Sealers for Your Business
Quality evaluation of vacuum pack sealers involves several practical steps. Start by reviewing third-party certifications or compliance with industry standards, such as ISO or FDA certifications, which can assure you of product safety and reliability.
Next, request samples or demonstrations. This allows you to assess the machine's performance firsthand, including sealing effectiveness and user-friendliness. During the demonstration, pay close attention to the sealing consistency, speed, and ease of operation.
Additionally, consult customer reviews and case studies from other businesses in your industry. Real-world feedback can highlight potential issues and advantages that may not be evident in specifications alone.
Finally, consider the manufacturer’s reputation. A supplier like XM XIEFA, with a solid background in food packaging, can offer insights into product performance and optimal usage scenarios, further enhancing your evaluation process.