Key Specifications for Vacuum Pack Food Machines

Contact Sales

Talk To Our Expert

Talk To Our Expert

Name
Email
Mobile
Message
0/1000

machine to vacuum pack food

Vacuum packing food is a vital process in food  packaging  that enhances shelf life and preserves freshness. For  businesses in retail, food  service, and  manufacturing, investing  in a  reliable machine  to vacuum  pack food  is  essential. This article will address key specifications,  cost factors,  installation guidance,  quality standards,  and the benefits of  advanced materials in vacuum  packing  technology to  help purchasing managers and food packaging professionals make  informed decisions.
Our Products

Key Specifications for Industrial Vacuum Packing Equipment

When selecting a  machine to vacuum pack food, several key specifications are crucial  for optimal performance. First, consider  the vacuum pump's capability, which directly  influences the machine's efficiency in removing air. A higher pump  capacity typically  means faster and  more effective vacuum sealing, which is vital for maintaining food quality.

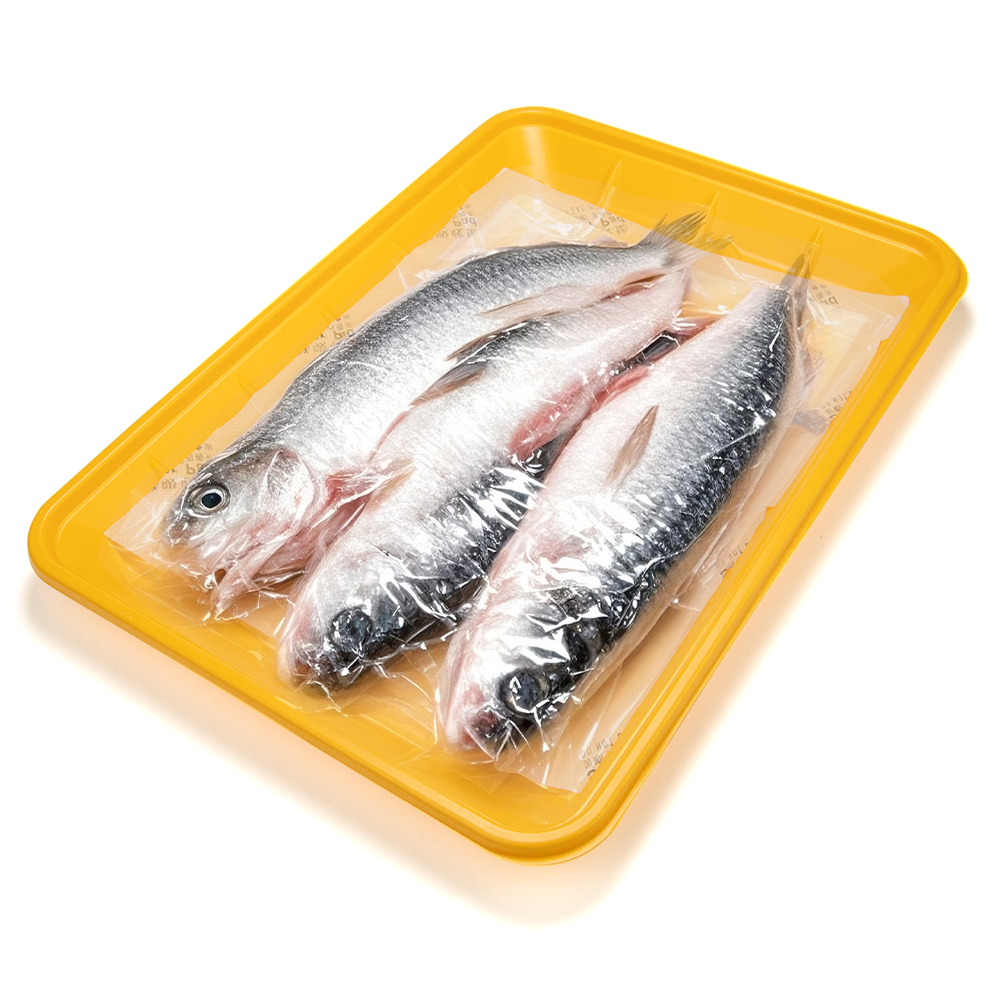
Next, look at the sealing width  and  length.  Wider seals create a more robust barrier against moisture and air, which is essential for preserving food items. Additionally, consider the material the machine can handle—many vacuum packers accommodate various packaging  films,  such as multi-layer plastics that provide superior barrier  properties. For example, our Factory wholesale food-grade EVOH paper trays for disposable packaging offer excellent moisture resistance.

Temperature control is another  significant specification. Advanced machines often feature adjustable temperature settings,  allowing for customization based on the type of food being packaged.  Certain  products, like delicate items or those sensitive to heat, require lower sealing temperatures  to prevent damage.

Lastly, evaluate the machine’s operating speed and cycle time. This is particularly important for businesses with high-volume packaging needs. A machine that  can operate quickly without sacrificing quality enhances overall efficiency.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Related product categories

Understanding the Cost Factors of Vacuum Pack Food Machines

Understanding the Cost Factors of Vacuum Pack Food Machines

The cost of a machine to vacuum  pack food can vary widely based  on several factors. One of the primary considerations is the machine’s capacity and specifications. Higher-capacity machines with advanced features generally come with a higher price tag, but they often provide  better efficiency and longer service  life, making them a worthwhile investment for  large operations.

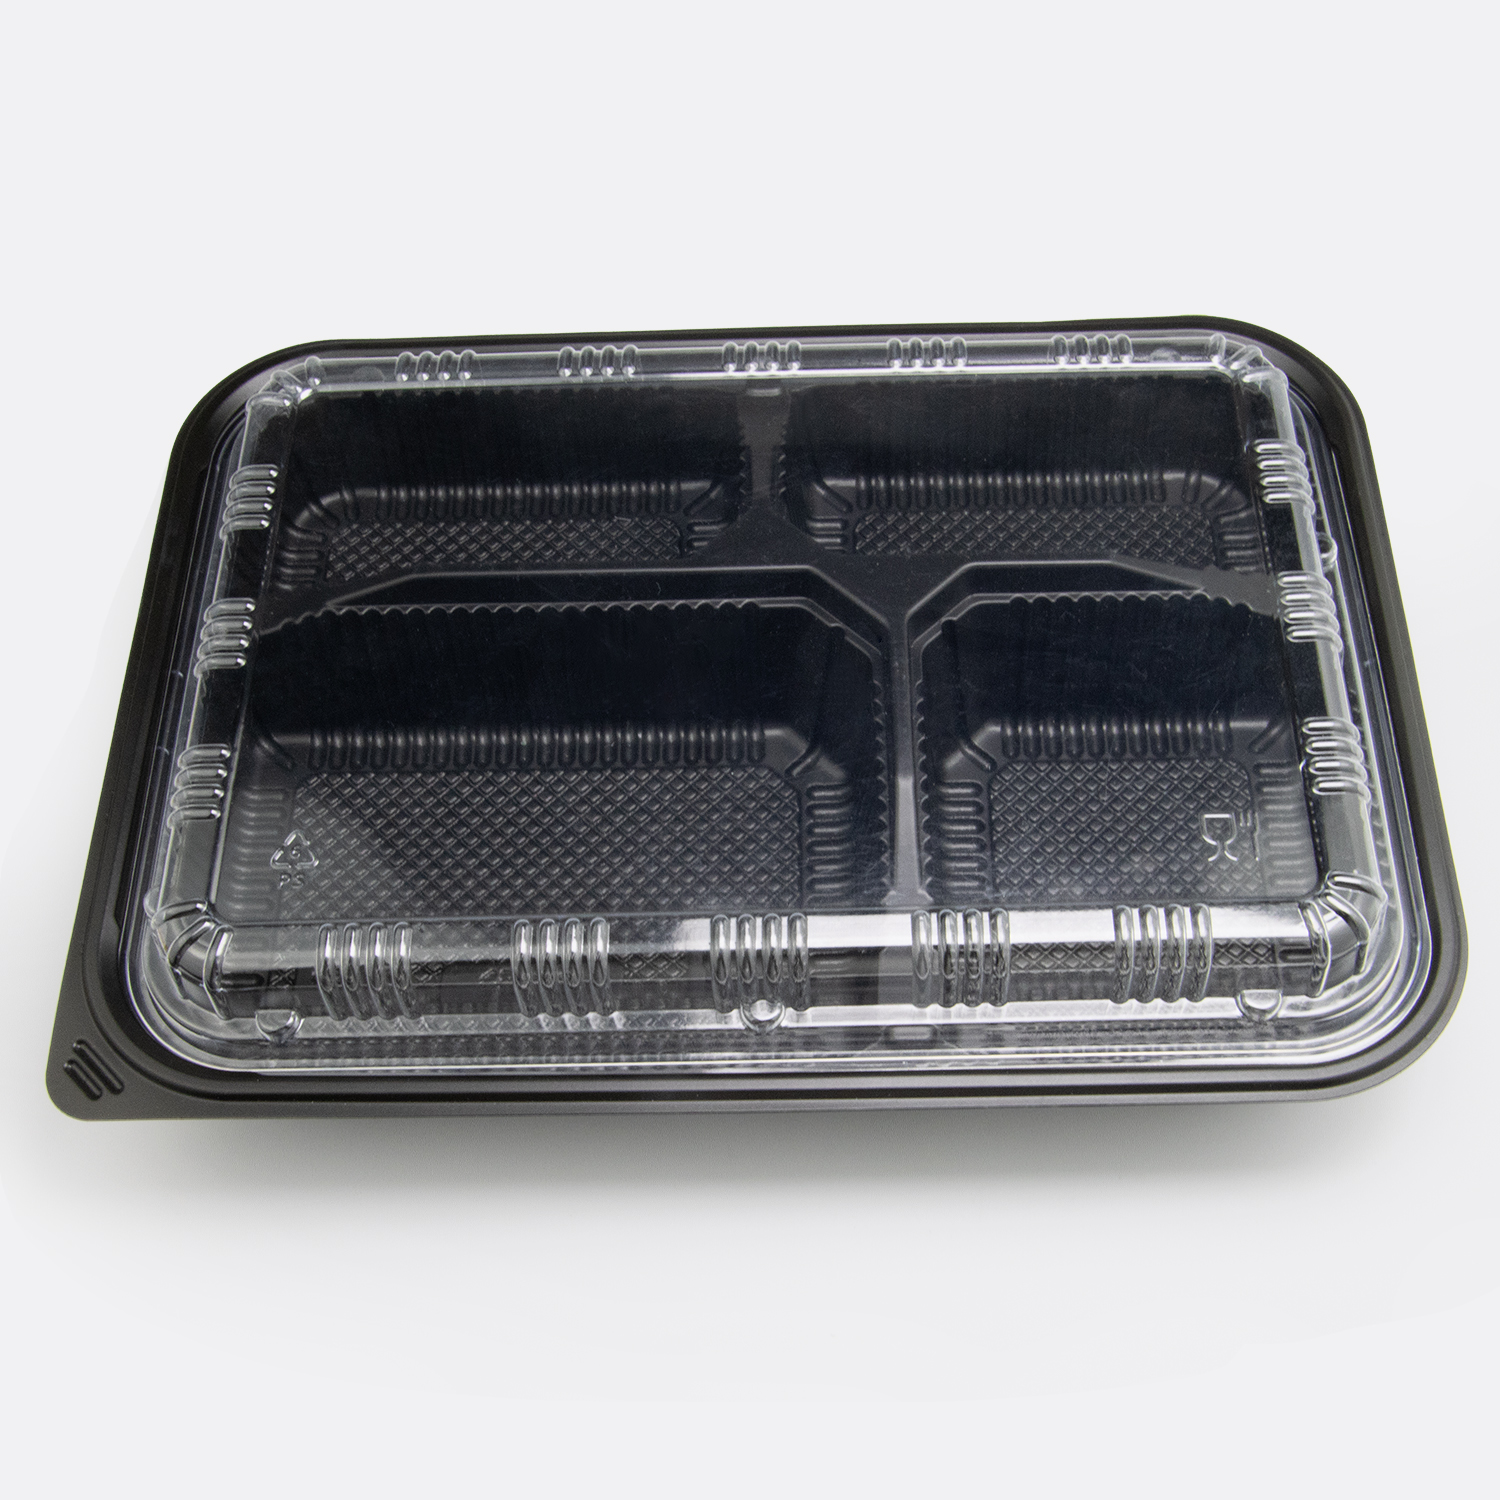
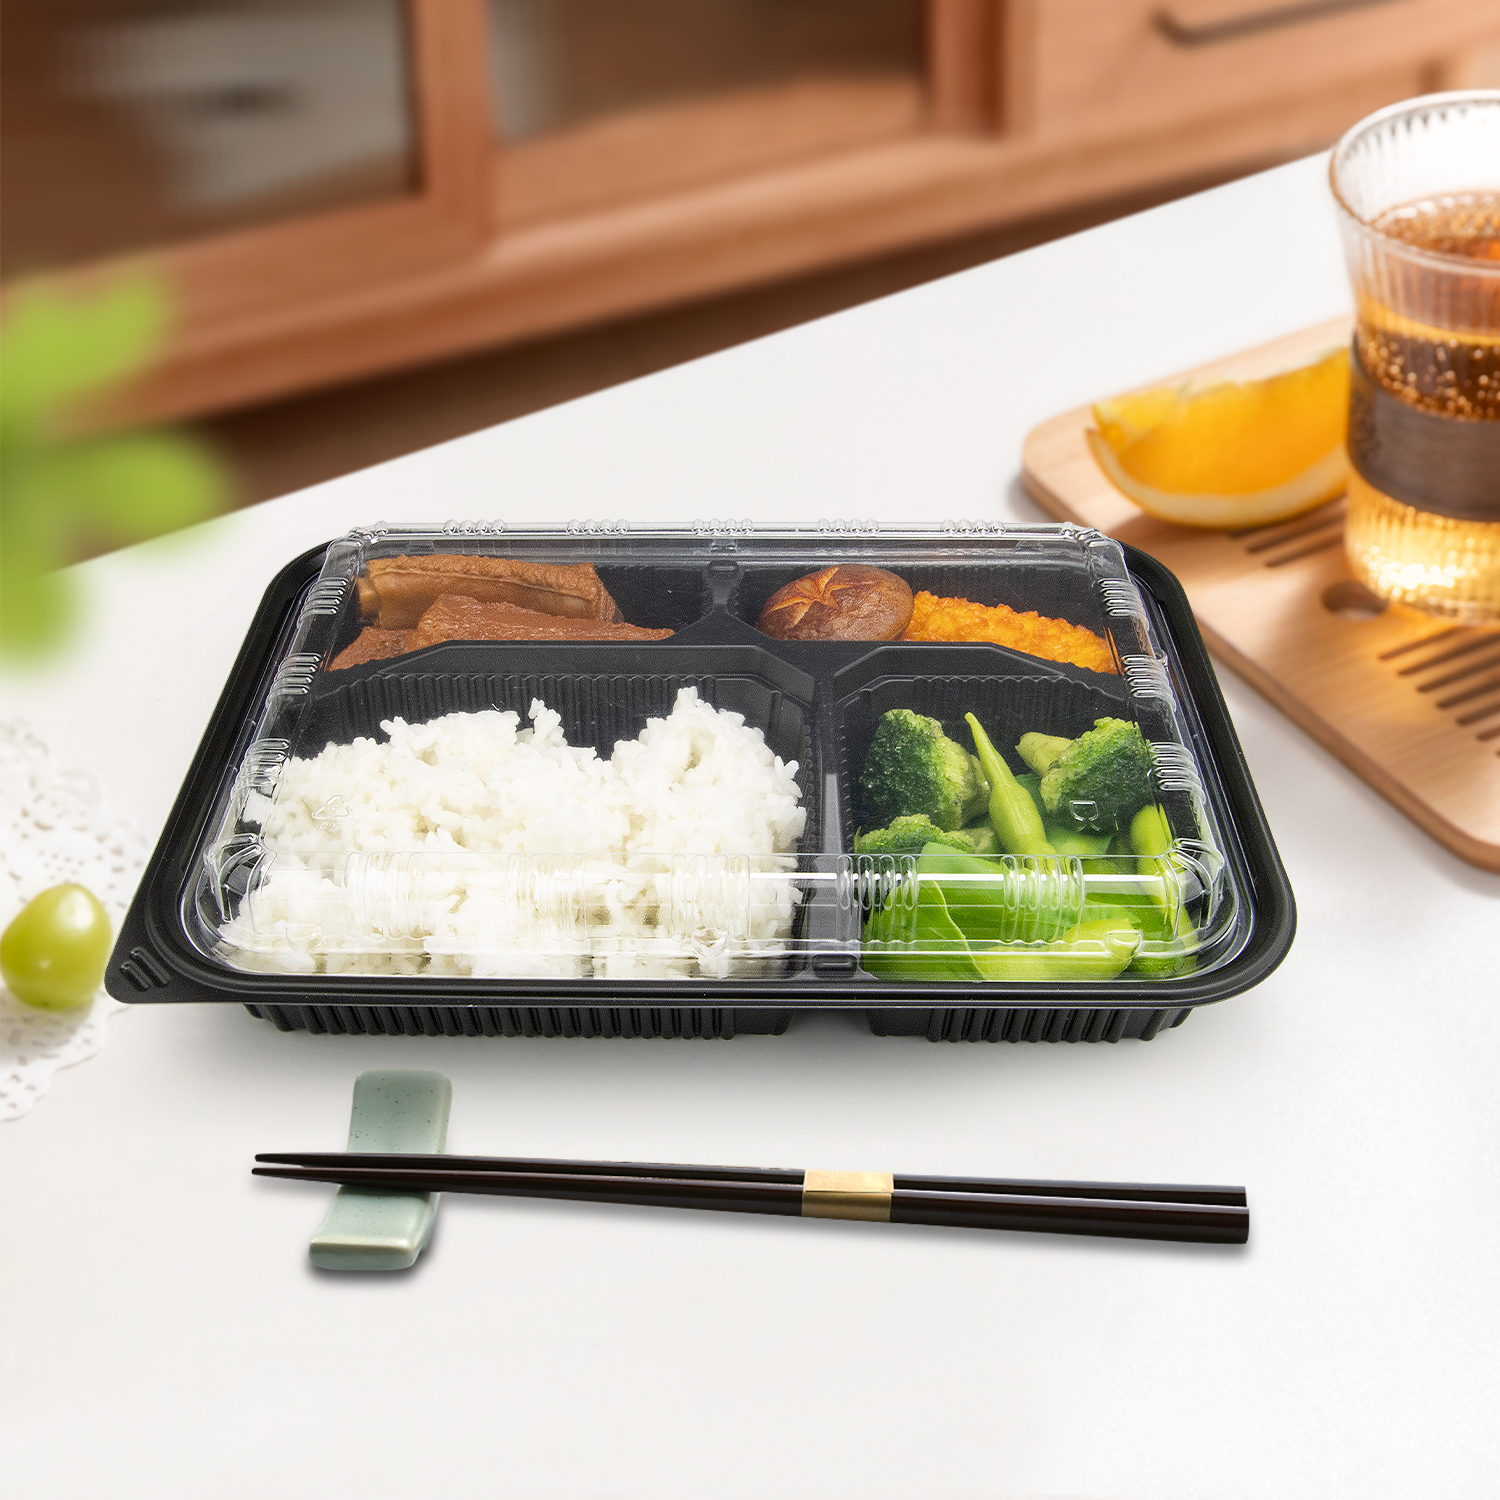
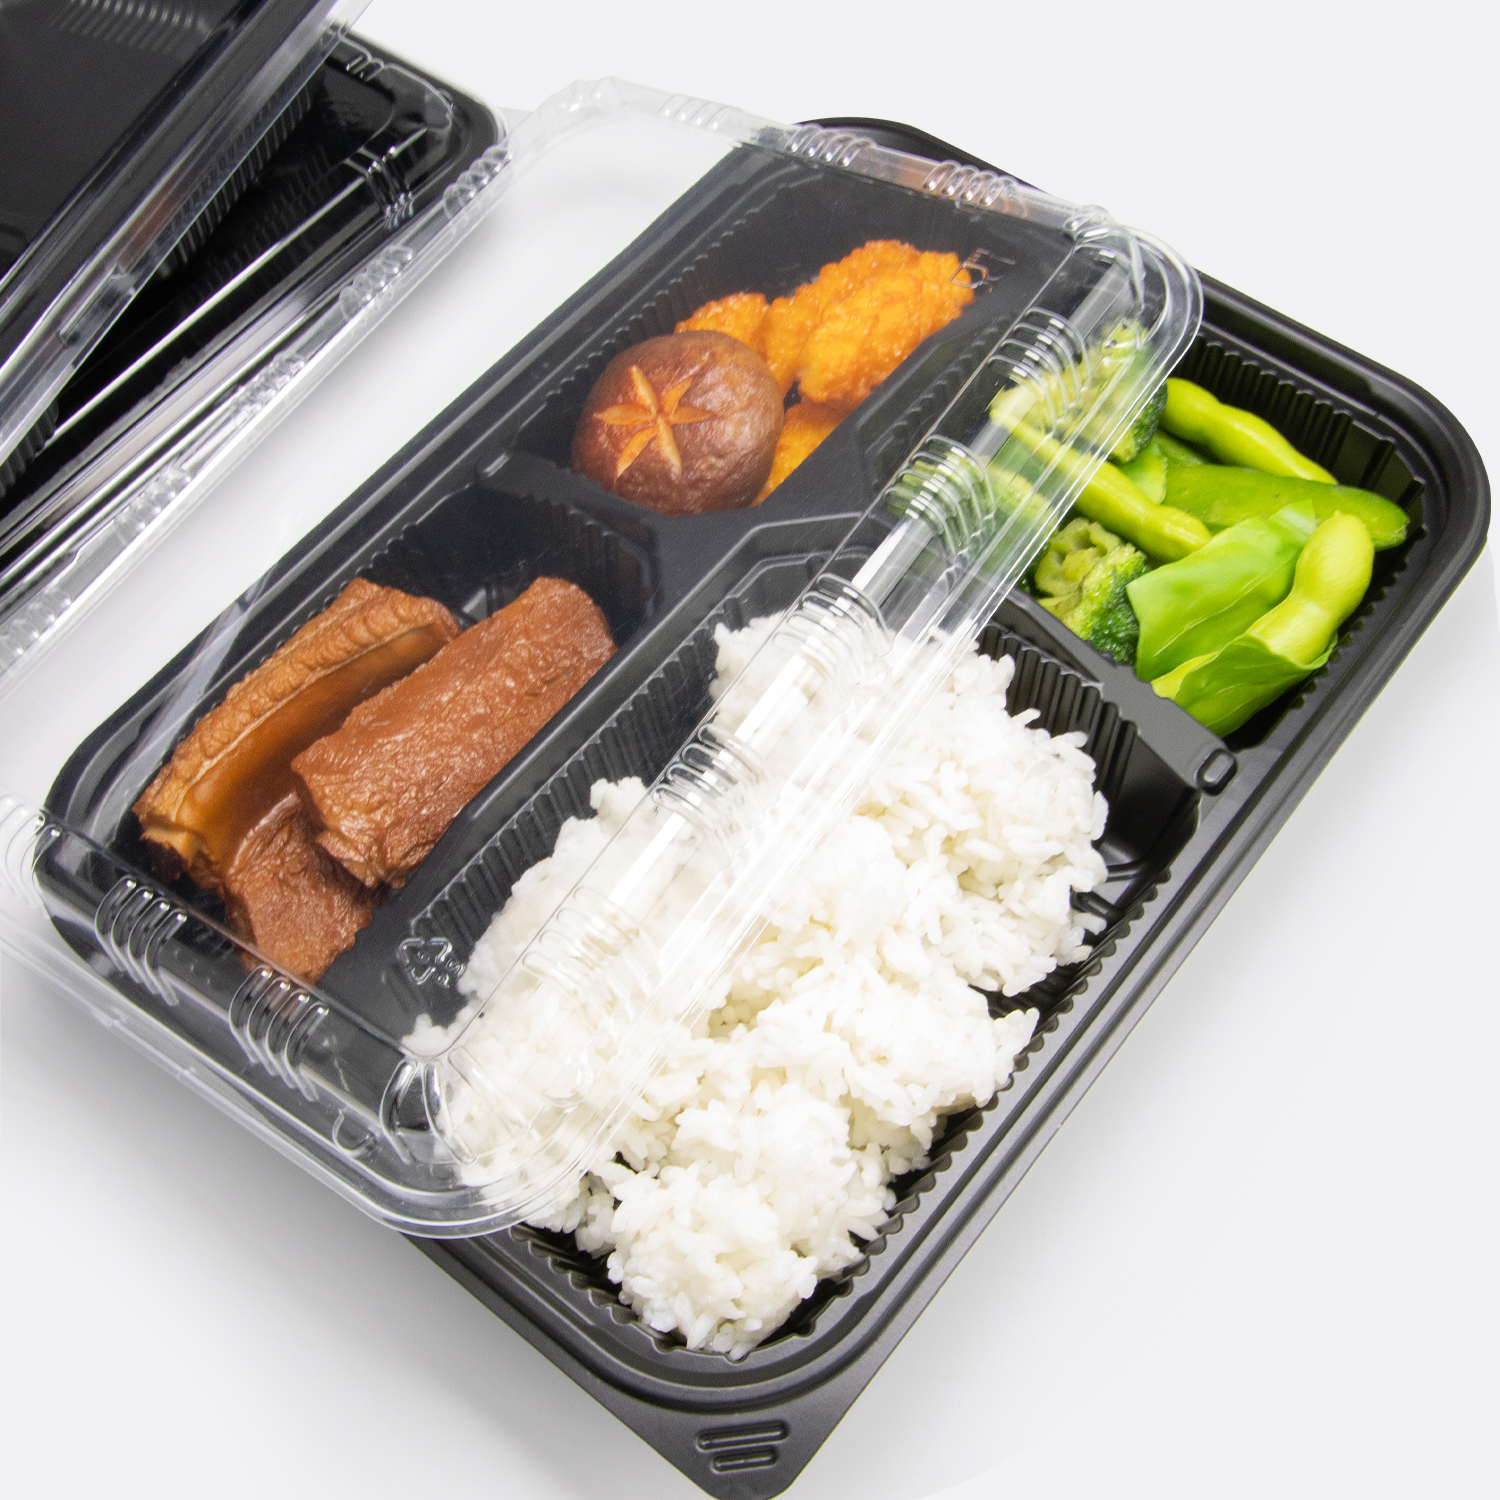
Another significant  cost factor is the material compatibility. Machines designed to work with specialized packaging materials may incur  additional costs, but these materials often  offer better protection for the  food, extending shelf  life and reducing waste. For instance, a 4-compartment PP takeaway food container with clear PET lids can be an excellent choice for preserving food quality.

Maintenance costs are also crucial to  consider. While some machines may have a lower initial purchase price, they might  require more frequent repairs or  replacement parts, leading to higher  long-term expenses. Choosing a machine from a reputable supplier with strong customer support and available parts can mitigate these costs.

Lastly, don’t forget  to factor in the potential return on investment (ROI). A  reliable vacuum packing solution can significantly reduce  food  spoilage and waste, leading  to considerable savings over time. Understanding these cost factors  will help you budget effectively and choose the right equipment for your business.
Installation Guidance for Efficient Vacuum Packing Solutions

Installation Guidance for Efficient Vacuum Packing Solutions

Proper installation  of your vacuum packing machine is critical to  achieving optimal performance. Begin by selecting a suitable location that is well-ventilated and  has easy access to  power sources. Ensure that the surface is level and  sturdy enough to support the weight of the machine, as this will help maintain accuracy during  operation.

Before installation, review the manufacturer's guidelines thoroughly. These will provide essential details regarding electrical requirements and  any necessary adjustments before the machine can be used. Additionally, ensure  that all safety features, such as emergency shut-off switches, are properly  installed and  functional.

It’s also  advisable to conduct a test run after installation. This  allows  you to check for any potential  issues  and confirm  that the vacuum packing machine operates correctly. Testing  with various  types  of food products can help ensure that you achieve optimal sealing  and vacuum levels, tailored to your specific operational needs.

Evaluating Quality Standards in Food Vacuum Packing Machines

Evaluating Quality Standards in Food Vacuum Packing Machines

Quality standards  are paramount when selecting a machine to vacuum pack food.  Look for equipment that complies with international food safety regulations, such as NSF  or  FDA certifications. These certifications ensure that  the  materials used are safe for food contact and  that the machine meets stringent hygiene requirements.

Additionally, consider the manufacturer's quality control processes.  A supplier with robust quality assurance practices,  including  thorough testing of machines before shipment, can reduce the  risk of operational issues and enhance product reliability.

It’s also beneficial to inquire about user feedback and performance history.  A  machine  with positive reviews regarding durability and performance in real-world applications can  provide  assurance of  its quality.  Engaging with other users or industry professionals can offer insights  into potential challenges and advantages of specific models.

Benefits of Advanced Materials in Vacuum Packing Technology

The use of advanced materials  in vacuum packing  technology can significantly enhance the preservation of food products.  Multi-layer films, for example,  provide excellent barrier  properties against moisture, oxygen, and light,  which are all critical factors in food degradation. These materials can  help extend the shelf life of packaged goods, reducing spoilage and waste.

Furthermore, advanced materials can improve the overall  appearance  of the packed product.  Clear, high-gloss  films not only enhance the visual  appeal but also provide a protective  layer that prevents physical damage during handling and transportation.

Buyers should also  consider the environmental impact of packaging materials. Innovations in biodegradable and recyclable films are becoming increasingly  available, allowing businesses to adopt sustainable practices without compromising food safety. These materials can align with corporate responsibility goals  while  appealing to environmentally conscious consumers.

Understanding the specifications, costs, installation, quality standards, and benefits  of  advanced materials can significantly influence the purchasing decision for a  machine to vacuum pack food. By carefully evaluating these factors, B2B buyers can select the right equipment to enhance their packaging processes, ultimately leading to better product preservation and customer satisfaction.